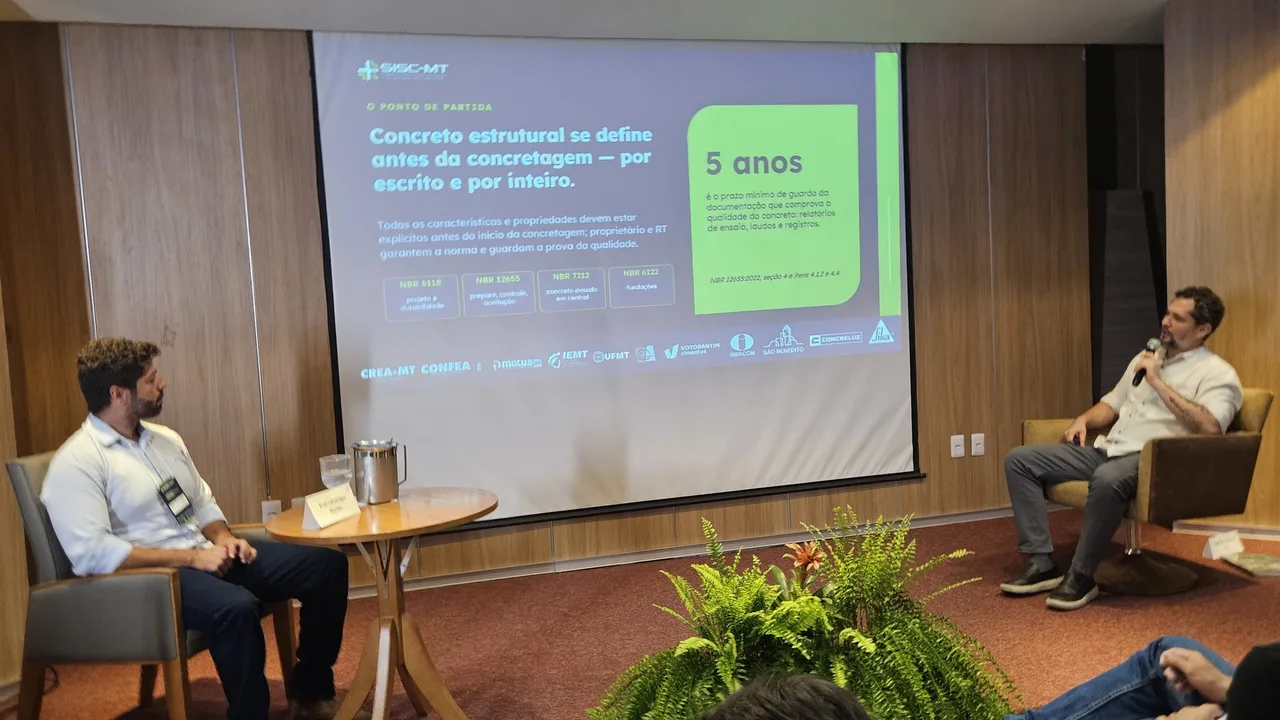
Structural concrete is defined before placement, in writing and in full. That was the opening line of the lecture I gave at the 1st SISC-MT. The claim is simple: if the order to the plant is only a strength class and a slump, later control inherits a poorly defined object.
What is missing when the order is only “C30, slump 12”
In the talk I used a recurring example. It is no use ordering an fck of 30 and a slump of 12 and then meeting excessive deflection in the member, if the modulus of elasticity never entered the specification. The concrete technologist has to understand, clearly, what that concrete needs, together with the structural designer and the site engineer, and close a complete specification: the mandatory items and the complementary ones.
Brazilian standard ABNT NBR 12655:2022, in section 4, sets out the duties along that chain. The professional responsible for the structural design defines the fck, the properties tied to durability and the special properties. The professional responsible for execution defines the method of production, the consistency and the maximum aggregate size, together with receiving and acceptance. The ready-mix company answers for the production stages of concrete batched at a central plant, within the scope of ABNT NBR 7212. The technologist, when engaged, supports mix design, control and the interface between design, site and plant. That professional title, on its own, does not replace the responsibilities the standard assigns to the other parties.
ABNT NBR 12655:2022 and ABNT NBR 7212 form the frame for production, the order, control and acceptance. Durability and cover requirements come, in addition, from ABNT NBR 6118. There is no need to turn every order into a universal list of tests. What matters for that member (modulus, control age, placing, density, temperature, or another special property) has to be written down before placement.
Variation is not a one-off defect
Every industrial product varies, and concrete does too. At the plant, that variation comes from several fronts at once: the materials (cement, aggregates, admixtures and additions), the internal process (batching by mass or by volume, calibration of the equipment) and the operation of the day. As I noted at the symposium, the concrete industry is harder to control than a closed production line, precisely because it combines several supplies and a continuous production process.
When the production unit does not yet have enough history, ABNT NBR 12655:2022, in item 5.6.3.3 and Table 7, sets the standard deviation to adopt when calculating the mix-design strength, according to the batching condition of item 5.6.3.1:
- condition A, applicable to all classes: cement and aggregates measured by mass, water measured by mass or by volume with a batching device and corrected for the moisture of the aggregates (standard deviation of 4.0 MPa);
- condition B, applicable to classes C10 to C20: cement by mass, water by volume with a batching device and aggregates by mass combined with volume (5.5 MPa);
- condition C, applicable only to classes C10 and C15: cement by mass, aggregates and water by volume, with the water corrected from an estimate of moisture and from consistency (7.0 MPa).
The mix formula in the standard itself is fcmj = fckj + 1.65 × sd (item 5.6.3). If the plant already has a known standard deviation, the value must be fixed from at least 20 consecutive results within 30 days, and never below 2 MPa (item 5.6.3.2). The batching condition is therefore not a plant detail: it weighs on the mix and, further on, on the lot acceptance coefficients as well.
In the lecture I recalled the three levels from memory and rounded condition B to 5 MPa. The value in the standard, checked in the 2022 edition, is 5.5 MPa, with the class limits above. The text of the standard holds, not the rounding in the talk.
Accepting the lot is not monitoring the process
ABNT NBR 12655:2022 organizes strength control by lot. There is total sampling, in which each batch is a lot and fck,est is the strength of the exemplar (the sample result) of that batch, and partial sampling, with different rules for 6 ≤ n < 20 and for n ≥ 20 (items 6.2.3.1 and 6.2.3.2). That apparatus serves to accept or reject that volume.
What the standard settles, then, is the point judgment of the lot. What production management needs is another reading: history, trend and variability, so as to act before the next failure. Tools such as Shewhart charts, CUSUM and stratification by plant, mix, laboratory or shift do not replace acceptance under the standard. They try to anticipate the problem, rather than only recording it afterwards.
In the lecture I showed an illustrative example for exactly that purpose: a series in which the individual results still fall inside the limits of a Shewhart chart, while the cumulative sum already indicates a drop. Those numbers were didactic. They were not a result from a job. They should not be read as evidence of a real case.
A poor test specimen still has to be investigated
A poor result on a test specimen is not, automatically, poor concrete. As I point out in the lecture, the cause may lie in molding, in storage or in the compression test. If the problem really is the concrete, the origin still has to be found: a change in the materials that went unnoticed, a failure in batching, or a change in the mix-design sheet that passed unseen.
The right sequence is to investigate, with traceability, before concluding. That holds for the producer and also for the site that uses concrete continuously over months. Looking only at the isolated point shows whether the problem has already happened. Following the process helps to see where it sits and how likely it is to happen again.
In practice
Before placement, write down what that concrete has to meet, beyond fck and consistency, whenever the function of the member requires it. At the plant, treat the batching condition and the standard deviation as a mix-design decision, not as an operational detail. On site and in the laboratory, when an exemplar fails, investigate the test and the production before assigning the cause. And do not confuse lot acceptance with the permanent monitoring of production.
The recording of the lecture, with the passage on specification from 19:55, is on the channel of the Instituto de Engenharia de Mato Grosso (Institute of Engineering of Mato Grosso): https://www.youtube.com/watch?v=o2Gic4EOv84&t=1195s.
References
- FIORESE NETO, Olivio. Especificação do concreto: gestão e controle da qualidade. Lecture. In: SISC-MT: Simpósio de Sustentabilidade e Tecnologia do Concreto (Symposium on Sustainability and Concrete Technology), 1st, 2026, Cuiabá. Recording: Instituto de Engenharia de Mato Grosso, 6 Nov. 2026. Available at: https://www.youtube.com/watch?v=o2Gic4EOv84. Accessed: 12 Nov. 2026.
- ABNT. NBR 12655: Portland cement concrete: Preparation, control, receiving and acceptance. Procedure. 4th ed. Rio de Janeiro: ABNT, 2022. Items 4, 5.6.3, 5.6.3.1 to 5.6.3.3, Table 7, 6.2.3. Checked for this text against the copy held under the CONFEA/CREA/Mútua system agreement.
- ABNT. NBR 7212: Concrete batched at a central plant. 2024 edition, with a 2025 correction, cited on the lecture slide as the standard for centrally batched concrete and for the order to the plant. No prescriptive items are taken from it here beyond that framing.
ABNT NBR 5738 and ABNT NBR 5739 were neither cited in the excerpt of the talk nor checked in the text for this article, so they are not entered as normative references.